In the field of sheet metal processing, bending is a crucial process that significantly impacts the final quality and functionality of sheet metal products. As a sheet metal bending supplier, I've encountered various common mistakes in this process over the years. Understanding these mistakes and how to avoid them is essential for ensuring high - quality products and customer satisfaction.
Common Mistakes in Sheet Metal Bending
1. Incorrect Bend Angle
One of the most frequent mistakes is achieving an incorrect bend angle. This can occur due to inaccurate machine settings or improper tooling. When the bend angle is off, it can lead to parts not fitting together correctly during assembly. For example, if a component is designed to fit precisely into another with a specific bend angle, even a small deviation can cause significant issues. This may result in a loose or overly tight fit, affecting the overall structural integrity of the final product.
2. Springback
Springback is a natural phenomenon in sheet metal bending. After the bending force is removed, the sheet metal tends to spring back slightly, changing the bend angle from the initially formed one. Failure to account for springback can lead to parts that do not meet the required specifications. Different materials have different springback characteristics. For instance, stainless steel generally has a higher springback compared to mild steel. If not properly compensated for, the final bend angle will deviate from the design, causing problems in subsequent assembly operations.
3. Material Cracking
Material cracking is another critical issue. It can happen when the bending radius is too small for the thickness and type of the sheet metal. When the metal is bent beyond its ductility limit, cracks may form at the bend area. This not only weakens the part but also makes it unsuitable for use in most applications. For example, in automotive or aerospace components, cracked sheet metal parts can pose serious safety risks. Additionally, improper lubrication during the bending process can also contribute to material cracking, as friction can cause excessive stress on the metal surface.

4. Twisting and Distortion
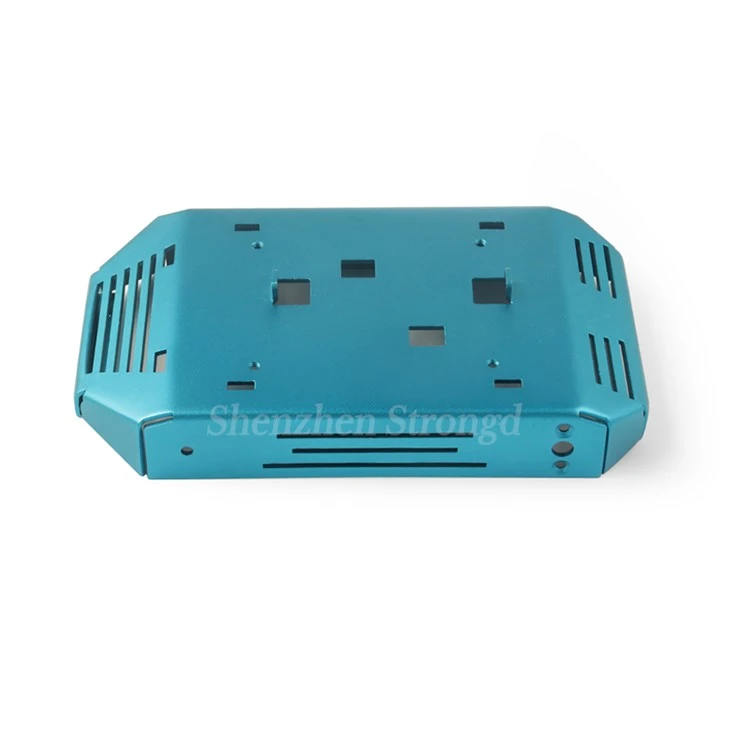
Twisting and distortion of the sheet metal can occur during bending, especially when the bending process is not properly balanced. Uneven pressure distribution on the sheet metal can cause it to twist or warp. This is often a problem when using older or poorly maintained bending equipment. Twisted or distorted parts are difficult to assemble and may require additional processing or even be scrapped, increasing production costs and lead times.
5. Inconsistent Bend Quality
Inconsistent bend quality means that the bends on different parts or even on different sections of the same part may vary in terms of angle, radius, or surface finish. This can be due to variations in the raw material, such as differences in thickness or hardness across the sheet. It can also result from inconsistent machine operation, such as fluctuations in the hydraulic pressure of a bending press. Inconsistent bend quality can make it challenging to ensure the interchangeability of parts, which is crucial in mass - production scenarios.
How to Avoid These Mistakes
1. Precise Machine Setup
To avoid incorrect bend angles, it is essential to have a precise machine setup. This includes accurately calibrating the bending press to ensure that the ram moves to the correct position and applies the right amount of force. Modern bending machines are often equipped with advanced control systems that allow for precise programming of bend angles and depths. Regular maintenance and calibration of the machines are also necessary to ensure their accuracy over time. Additionally, using high - quality tooling that is properly matched to the sheet metal thickness and bend requirements can significantly improve the accuracy of the bend angle.
2. Accounting for Springback
To compensate for springback, engineers need to have a good understanding of the material's properties. They can use empirical data or computer - aided engineering (CAE) simulations to predict the amount of springback. Once the springback amount is estimated, the bending process can be adjusted accordingly. For example, the initial bend angle can be set slightly larger than the desired final angle to account for the springback. Some advanced bending machines also have built - in springback compensation features that can automatically adjust the bending parameters based on the material type and thickness.
3. Appropriate Bending Radius Selection
To prevent material cracking, it is crucial to select an appropriate bending radius based on the material thickness and type. Generally, the minimum bending radius should be at least equal to the sheet metal thickness for most common materials. For more brittle materials, a larger bending radius may be required. In addition, using proper lubrication during the bending process can reduce friction and stress on the metal surface, further minimizing the risk of cracking.
4. Balanced Bending Process
To avoid twisting and distortion, a balanced bending process is necessary. This can be achieved by ensuring that the pressure is evenly distributed across the sheet metal during bending. Using fixtures and supports to hold the sheet metal in place can help maintain its stability. Some bending machines are designed with multiple cylinders or adjustable dies to provide more uniform pressure distribution. Regular inspection and maintenance of the bending equipment can also prevent issues related to uneven pressure caused by mechanical wear.
5. Quality Control Measures
To ensure consistent bend quality, strict quality control measures should be implemented throughout the production process. This includes inspecting the raw materials before processing to ensure their uniformity in terms of thickness, hardness, and surface finish. During the bending process, in - process inspections can be carried out at regular intervals to check the bend quality. Using measurement tools such as angle gauges and calipers can help detect any deviations from the specifications early on. Statistical process control (SPC) techniques can also be applied to monitor and control the production process, ensuring that the bend quality remains within the acceptable range.
Our Expertise as a Sheet Metal Bending Supplier
As a sheet metal bending supplier, we have extensive experience in dealing with these common mistakes. We use state - of - the - art bending equipment that is regularly maintained and calibrated to ensure high - precision bending. Our team of engineers is well - versed in the properties of different sheet metal materials and can accurately predict and compensate for springback. We also have a strict quality control system in place, from raw material inspection to final product testing, to ensure that every part meets the highest quality standards.
We offer a wide range of sheet metal bending services, including Sheet Metal Stamping Bending, Sheet Metal Cutting and Bending, and Bending Laser Cutting. Our advanced technology and skilled workforce enable us to handle complex bending requirements with ease. Whether you need simple bends for small - scale projects or intricate bends for large - scale industrial applications, we can provide customized solutions to meet your specific needs.
If you are looking for a reliable sheet metal bending supplier, we invite you to contact us for procurement and further discussions. We are committed to providing you with high - quality products, competitive prices, and excellent customer service. Let us work together to bring your sheet metal projects to life.
References
- ASM Handbook Volume 14A: Metalworking: Bulk Forming. ASM International.
- Tool and Manufacturing Engineers Handbook, 4th Edition. Society of Manufacturing Engineers.
- Bending and Forming of Sheet Metal: A Practical Guide. Industrial Press Inc.